

A Buyer’s Checklist for Cellulose Ether Consistency Across Production Batches
A Buyer’s Checklist for Cellulose Ether Consistency Across Production Batches
For procurement teams, consistent Cellulose Ether performance across production batches protects product quality, controls formulation risk, and prevents expensive production interruptions or project claims.
This checklist helps buyers assess specifications, supplier controls, test methods, documentation, and commercial safeguards before approving HPMC or related cellulose ether materials.
What Procurement Teams Are Really Trying to Prevent
Buyers searching for Cellulose Ether consistency are rarely looking for a basic product definition. They need confidence that today’s approved sample will match future deliveries.
A material can meet a broad specification while still behaving differently in a dry-mix mortar, detergent, coating, adhesive, ceramic, or chemical formulation.
Small shifts in viscosity, moisture, particle size, substitution level, dissolution behavior, or gel temperature can affect workability, water retention, thickening, and storage stability.
Those changes may force production operators to adjust water dosage, mixing time, additive levels, or process temperature, increasing labor and reducing formulation control.
For construction-material manufacturers, inconsistent cellulose ether may cause variable open time, sag resistance, slip resistance, bond strength, or application feel across finished batches.
For chemical and household-product manufacturers, inconsistency can create uneven viscosity development, poor dispersion, haze, sedimentation, foam changes, or consumer-facing appearance problems.
The procurement objective is therefore not simply obtaining the lowest unit price. It is securing a predictable input with controlled performance over the supplier relationship.
A capable supplier should demonstrate repeatable manufacturing, transparent quality systems, traceable records, and practical support when a delivered batch differs from expected behavior.
Start with Application-Critical Specifications
Do not approve Cellulose Ether based only on product grade names. Grade labels vary between suppliers and may conceal major differences in functional performance.
First identify the parameters that directly influence your finished product. These should become the basis of purchasing specifications, incoming inspection, and supplier comparison.
Viscosity is usually the first requirement to define. However, buyers must specify the measurement method, solution concentration, temperature, spindle, speed, and reporting unit.
A viscosity result measured under one method cannot be meaningfully compared with a result measured using another concentration or instrument setting.
Ask whether viscosity is controlled as a target, a broad range, or a minimum value. Broad ranges may be commercially convenient but technically risky.
For high-viscosity HPMC, even modest variation can affect water demand, mixing behavior, consistency development, and final application properties in sensitive formulations.
Moisture content should also be controlled because it influences handling, active material content, packaging stability, and the actual amount dosed into production.
For powdered products, particle-size distribution matters when rapid wetting, fast dissolution, low dust, or stable automated feeding performance is required.
Buyers should define whether the material must pass through a specified mesh size, meet a distribution profile, or achieve a maximum residue limit.
Other relevant criteria may include pH, ash content, methoxy content, hydroxypropoxy content, gel temperature, surface treatment, apparent density, and insoluble matter.
Not every application requires every test. The correct approach is to select the smallest set of specifications that reliably predicts finished-product performance.
Require a Clear Link Between Raw Material Tests and Formulation Results
A certificate of analysis is valuable, but it should not be the only evidence used for approval. Standard laboratory values may miss application-specific performance changes.
Procurement should work with technical teams to identify one or two practical formulation tests that detect meaningful batch variation quickly.
For tile adhesive, these may include water retention, slip, open time, tensile adhesion, consistency after standing, and workability at fixed water addition.
For skim coat or gypsum products, suitable checks may include water demand, spreading behavior, thickening rate, surface finish, cracking tendency, and retarder compatibility.
For detergents and chemical blends, useful tests often include hydration time, solution clarity, viscosity build, salt tolerance, suspension stability, and storage behavior.
A supplier sample should pass both its technical data sheet limits and your representative formulation test before it receives full production approval.
Document the exact formula, mixing sequence, water temperature, equipment, mixing speed, test timing, and acceptance criteria used during qualification testing.
Without standardized test conditions, buyers may incorrectly attribute normal process variation to the Cellulose Ether supplier or overlook a genuine material difference.
Retain comparison samples from approved lots whenever practical. These reference samples make it easier to investigate future deviations objectively and quickly.
Examine How the Supplier Controls Batch-to-Batch Variation
Consistency begins before final quality inspection. Buyers should understand whether the supplier controls critical variables throughout production rather than sorting problems at shipment.
Ask how raw materials are qualified, how substitution reactions are monitored, and how process conditions are maintained across reactors, shifts, and production lines.
A manufacturer with integrated production control can usually manage variability more effectively than a trading source with limited visibility into actual manufacturing conditions.
Automated dosing, monitored reaction conditions, standardized drying, controlled milling, and consistent blending procedures all reduce the risk of lot-to-lot performance drift.
However, automation alone does not guarantee reliable quality. Buyers should also ask about calibration, preventive maintenance, deviation management, and trained quality personnel.
Find out whether final batches are blended to a target profile. Controlled blending can improve uniformity when applied with documented procedures and verified results.
Request information about the number of manufacturing sites and production lines supplying your grade. Multi-site supply requires strong cross-site standardization and validation.
When a supplier changes a plant, production line, process, raw material source, or packaging format, the buyer should receive advance written notification.
This requirement should apply even when the supplier believes the product specification remains unchanged. A technically equivalent grade may still require formulation confirmation.
Suppliers with annual capacity, stable process knowledge, and a broad viscosity-control range may offer stronger supply resilience, but qualification evidence remains essential.
Check Certificates of Analysis Beyond the Numbers
A certificate of analysis should identify the product, production batch, manufacturing date, test date, packaging date, quantity, and relevant release specifications.
Every reported result should be traceable to a defined test method. Generic statements such as “qualified” provide less value than measurable recorded results.
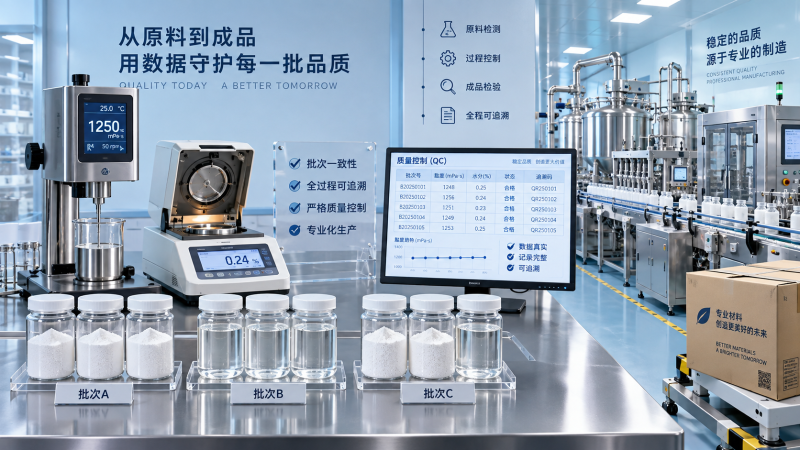
Review several certificates from different production dates, not just one recent document. This reveals whether results consistently cluster near expected target values.
Pay particular attention to results frequently close to specification limits. Repeated edge-of-range results may indicate insufficient process capability for your application.
Ask whether the certificate reflects testing from the final blended batch or a sample collected earlier in the process before packaging and release.
For strategic materials, request historical trend data for viscosity, moisture, ash, and other critical parameters. Trend charts can reveal gradual drift before failures occur.
Also confirm the supplier’s retention-sample policy. A retained sealed sample from each batch supports fair investigations when quality disputes arise later.
Certificates should be issued consistently in the agreed language and format. Procurement systems work better when documents can be matched automatically to receiving records.
Validate Packaging, Storage, and Delivery Controls
Even a well-manufactured Cellulose Ether can lose usability when packaging fails to protect it from moisture, contamination, or prolonged unsuitable storage conditions.
Confirm bag construction, inner liner quality, sealing method, net weight tolerance, pallet configuration, labeling, and whether packaging suits your warehouse handling system.
Each package label should show the product name, batch number, production date, net weight, storage guidance, and supplier identification clearly enough for receiving teams.
Inspect initial deliveries for damaged bags, powder leakage, inconsistent labeling, pallet instability, and visible evidence of moisture exposure during transport or storage.
Specify the remaining shelf-life required at delivery. This is especially important for import shipments, long transit routes, distributor stock, and seasonal purchasing cycles.
Agree on storage recommendations that match your site conditions. Warehouses with high humidity, temperature fluctuations, or open loading areas need extra controls.
Delivery consistency also includes lead-time reliability. A supplier that maintains quality but regularly misses delivery windows can still disrupt production planning and customer commitments.
Build a Practical Incoming Inspection Plan
Incoming inspection should be risk-based. Testing every parameter on every bag is usually unnecessary, but relying only on supplier paperwork creates avoidable exposure.
Set receiving rules for identity confirmation, package condition, batch documentation, random sampling, quick moisture checks, and periodic viscosity or application verification.
For new suppliers, newly approved grades, or critical formulations, increase test frequency until enough data demonstrates stable and repeatable delivered performance.
Once performance is proven, a reduced inspection plan may be appropriate. The plan should still trigger enhanced testing after complaints, process changes, or unusual results.
Sampling must be representative. Powder segregation can occur during filling, transport, and storage, so samples should be taken according to a documented method.
Train warehouse and laboratory personnel to recognize lot-mixing risks. Different batches should remain identifiable until released and should not be combined without authorization.
Establish a quarantine process for questionable deliveries. Material should remain isolated while procurement, quality, and technical teams review the evidence and decide disposition.
Assess Supplier Response When Something Goes Wrong
Quality problems cannot always be eliminated, so buyers should evaluate how a supplier investigates and resolves nonconformities before placing large recurring orders.
Ask for the supplier’s complaint process, expected response time, root-cause methodology, corrective-action format, and policy for replacement or credit decisions.
A useful investigation compares the complaint sample, supplier retention sample, production records, test methods, shipment conditions, and relevant formulation results.
Suppliers should not simply state that the certificate met specification. They should help determine whether the specification itself failed to protect your application.
For important accounts, define escalation contacts across sales, quality assurance, technical service, and logistics. A single sales contact is rarely enough during a production stoppage.
Include change-notification and complaint-response expectations in supply agreements. Written controls reduce ambiguity when commercial pressure is high and fast decisions are required.
Compare Suppliers on Total Cost, Not Price Per Kilogram
The lowest Cellulose Ether price can become expensive when inconsistency raises water demand, increases rework, causes rejected finished goods, or triggers customer complaints.
Compare suppliers using delivered cost, formulation dosage, quality-control workload, yield impact, storage losses, payment terms, lead times, and technical support capability.
A slightly higher-priced product may reduce total cost when it delivers stable rheology, predictable processing, lower dosage variation, and fewer emergency production adjustments.
Run side-by-side trials using equivalent functional targets rather than equal dosage only. The cheapest grade at one dosage may not be cheapest at required performance.
For detergent and chemical formulations, consider application-specific options such as Detergent-grade HPMC when evaluating hydration, thickening, clarity, and formulation compatibility.
Do not treat capacity claims as a substitute for quality evidence. Capacity matters for supply continuity, but batch consistency must be demonstrated through data and trials.
Use This Approval Checklist Before Signing a Supply Agreement
Before approval, confirm the grade’s identity, application purpose, target viscosity, testing method, moisture limit, particle-size requirement, and other critical functional parameters.
Verify that supplier certificates contain batch traceability, actual test values, release methods, manufacturing details, and consistent documentation suitable for your internal quality system.
Review multiple production batches, not just qualification samples. A meaningful trial should include enough lots to reveal normal manufacturing variation and operational repeatability.
Confirm packaging, shelf life, logistics capability, storage suitability, and contingency arrangements for delayed deliveries or unexpected demand increases.
Require documented change control covering manufacturing sites, raw materials, process steps, test methods, product specifications, and packaging materials that could affect performance.
Agree on complaint handling, retained samples, corrective-action expectations, commercial remedies, and named technical contacts before an issue creates urgency.
Conclusion: Consistency Is a Purchasing Requirement, Not a Hope
Reliable Cellulose Ether sourcing depends on more than selecting a recognized grade or accepting a supplier’s standard certificate of analysis.
Procurement teams should define application-critical specifications, validate formulation behavior, examine supplier process control, and maintain traceability from delivery through finished-product release.
When these controls are built into qualification and supply agreements, buyers gain better cost predictability, fewer production disruptions, and stronger confidence in every production batch.
Send Your Inquiry
We welcome your cooperation and we will develop with you.
