

CAS 9004-65-3 in Construction Formulations: Which Technical Parameters Matter Most?
Start with the parameter sheet, not the product name
For technical assessors, CAS 9004-65-3 is only the entry point. In construction formulations, what matters is how that cellulose ether behaves inside a specific system: tile adhesive, skim coat, wall putty, self-leveling mortar, gypsum-based mix, or EIFS-related material. Two samples can share the same CAS number and still perform very differently once you look at viscosity, substitution profile, particle size, moisture, pH, and batch consistency.
If the goal is a sound technical decision, treat evaluation as a checklist tied to application risk. The wrong grade usually does not fail on one headline parameter alone. It fails because one overlooked detail shifts water demand, delays hydration too much, shortens open time, or makes the mix unstable under site conditions.
Check viscosity in the context of the test method
Viscosity is often the first number people compare, and it is also one of the easiest to misuse. A quoted value means little unless you know the measurement conditions: solution concentration, temperature, spindle or instrument method, and whether the supplier is reporting Brookfield-type data or another lab setup. A 50,000 CPS grade from one source is not automatically interchangeable with a 50,000 CPS grade from another if the method is different.
In practice, assess viscosity against the job the material needs to do:
- Higher viscosity grades usually support water retention and anti-sag performance, but they can also raise mixing resistance and affect spreadability.
- Lower viscosity grades may improve flow and ease of mixing, yet they can leave the system short on open time or edge stability.
- In cement-based products, a grade that looks fine on paper can still create a sluggish feel if the formulation already contains strong water-demand components.
A common mistake is to rank candidates by viscosity alone. That is how teams end up with a mortar that mixes well in the lab but loses application comfort on site.
Do not skip substitution-related behavior
For HPMC used under CAS 9004-65-3, substitution characteristics strongly influence thermal gel behavior, water retention profile, and interaction with mineral binders. Many buyers ask for a target viscosity range and stop there. That is not enough when the formulation is sensitive to open time, slip resistance, or workability window.
You do not always need the full chemistry report to make a practical judgment, but you do need evidence of stable substitution control from the supplier. Ask for the grade definition behind the commercial name and compare trial results under the same formulation and same water addition. If one sample gives stronger initial body but poorer open time, while another holds water better but slows finishing, substitution differences are often part of the reason.
This is especially relevant when switching sources. “Equivalent grade” claims are easy to make and hard to prove without side-by-side formulation testing.
Match the grade to the application, not to a generic category
Construction grade cellulose ethers are not interchangeable across all drymix systems. Technical assessment gets more reliable when the first question is not “What is your best-selling HPMC?” but “What is this formulation expected to tolerate?”
The point is simple: evaluate performance under the exact binder system and additive package you actually use. A technically strong grade in one mortar can be the wrong choice in another.
Look at water retention as a functional result, not a sales claim
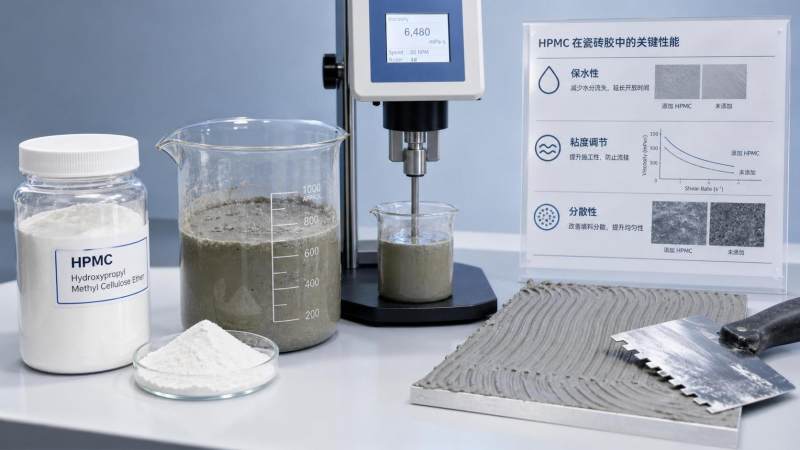
Water retention is one of the main reasons CAS 9004-65-3 matters in construction formulations, but the number only becomes meaningful when linked to substrate condition, ambient temperature, absorbency, and layer thickness. The same material can look excellent on a controlled panel and behave differently on a hot, porous wall.
During evaluation, check three things together: retained workability after mixing, surface drying rate during application, and end-use signs such as skinning, poor wetting, or weak bond development. Many teams focus on lab retention data and miss the application window. That is where complaints usually start.
Check particle size because it affects dispersion speed and mixing behavior
Particle size does not always get top billing, but it matters in daily production. A cellulose ether that disperses too slowly can create fish-eyes or gel lumps during mixing. One that wets too fast under the wrong process can also make batch preparation harder, especially where equipment shear is limited.
Ask how the material is intended to be added: dry blend first, then water; or introduced under a different sequence. Then test under your real mixing energy, not an idealized lab setup. This is one of those parameters that looks minor until it starts wasting operator time and creating uneven batches.
Review moisture content and flowability before blaming the formula
If incoming powder has unstable moisture or poor flowability, dosage control and dry blending consistency suffer. That can lead to variation that gets misread as a formulation problem. In production environments with humid storage or long transport routes, this checkpoint becomes more important.
A practical rule: when trial batches show unexpected spread in application feel, check the raw material handling side early. Packaging integrity, caking tendency, and powder movement through the feeding system are worth reviewing before you start rewriting the recipe.
Purity matters when side effects start showing up
For technical screening, purity is less about a marketing label and more about controlling unwanted interactions. Residual salts, by-products, or other non-functional content may affect odor, color, pH behavior, or compatibility with other additives. In some systems, you will barely notice it. In more sensitive formulations, it can show up as poorer stability or harder-to-explain performance drift.
When a sample passes basic viscosity and water retention checks but still creates inconsistent finish quality, purity-related differences should move up your review list.
Test compatibility with RDP, starch ether, and the binder package
This is where many technical evaluations become too narrow. CAS 9004-65-3 does not work alone in modern construction drymix. Its real value depends on how it interacts with redispersible polymer powder, starch ether, cement, gypsum, fillers, retarders, and specialty additives.
Run compatibility checks at realistic dosages. Watch for these warning signs:
- Unexpected thickening after a small formulation change
- Loss of flow when polymer level increases
- Good fresh-state feel but unstable open time
- Surface defects that appear only after replacing one additive supplier
If your company already works with broad cellulose ether and drymix solution ranges, this cross-effect testing should be standard practice rather than a troubleshooting step at the end.
Batch consistency is a technical parameter, even if it is not listed that way
A grade with a wide viscosity portfolio is useful only if lot-to-lot control is tight. For assessors, consistency is not a commercial afterthought. It determines whether the formulation can survive scale-up without constant water adjustment or operator compensation.
Ask for routine specification control points and compare more than one lot if the project matters. Short trials with a single sample often hide the real question: will the same formula still run smoothly after three shipments and different weather conditions in storage?
Use a tighter evaluation sequence
A practical assessment flow saves time:
- Confirm the test method behind the supplier’s viscosity data.
- Check whether the grade is positioned for your exact construction application.
- Run fresh-state tests focused on mixing, trowelability, sag, open time, and water retention.
- Review dispersion behavior and any particle-size-related mixing issues.
- Check compatibility against the full additive package, not the cellulose ether in isolation.
- Compare at least multiple lots if the formulation will move into stable production.
That sequence sounds basic, but it prevents a very common error: approving a grade because it looked fine in a narrow lab screen, then discovering later that the process window is too tight for manufacturing or jobsite use.
What usually deserves the most weight
If you need to prioritize, put the heaviest weight on parameters that change application outcome directly: viscosity under a defined method, substitution-related behavior, water retention performance in the target system, compatibility with the full formulation, and batch consistency. Particle size, moisture, and purity may look secondary, but they often explain why a promising grade becomes troublesome in production.
The right way to assess CAS 9004-65-3 in construction formulations is not to chase a single “best” number. Build the decision around the actual use case, verify the method behind every claimed parameter, and test under the same mixing and application conditions the product will face in the field. That is usually enough to separate a workable grade from one that only looks convincing on a data sheet.
Send Your Inquiry
We welcome your cooperation and we will develop with you.
