

Key Quality Tests for HPMC 200000 in Dry-Mix Mortar Production Control
Consistent dry-mix mortar performance starts long before a bag reaches the jobsite. It begins with disciplined incoming-material control, especially when a high-viscosity cellulose ether such as HPMC 200000 is used to govern water retention, open time, sag resistance, and application feel.
For quality-control and safety teams, a single viscosity value is not enough to release a batch. A material may appear compliant on a certificate of analysis yet still create trouble in production if its moisture level, pH, particle-size distribution, dissolution profile, ash content, or lot-to-lot stability has shifted. In cement- and gypsum-based formulations, those small shifts can become visible as unstable water demand, reduced workability, uneven thickening, poor trowel response, or complaints from applicators.
This article outlines the key quality tests used to control HPMC 200000 for dry-mix mortar manufacturing, explains what each result means in practical terms, and highlights how to build a release process that supports both product consistency and safe handling.
Start by Defining What “200000” Actually Means
In construction chemicals, “200000” normally refers to a nominal viscosity grade, commonly expressed in mPa·s or CPS. However, viscosity values cannot be compared responsibly without knowing the test conditions. HPMC viscosity depends on polymer concentration, solution preparation method, test temperature, spindle or measuring system, shear condition, and hydration time.
A quality specification should therefore state more than “HPMC 200000 CPS.” It should identify the solution concentration used for the test, the temperature at measurement, the instrument method, and the acceptable tolerance range. Without these details, two laboratories may obtain very different results from the same sample and mistakenly treat the difference as a quality problem.
For production control, the objective is not simply to obtain the highest viscosity. The objective is to obtain the viscosity profile that matches the approved mortar formula. A grade that is slightly higher than expected may produce overly stiff mixes or slow down wetting. One that is lower may weaken water retention or reduce anti-sag performance in tile adhesive, skim coat, repair mortar, or plaster.
The Incoming Inspection Tests That Matter Most
A practical inspection plan combines identity confirmation, physical testing, solution testing, and comparison against retained reference material. The exact limits should be tied to the approved formulation and supplier agreement, but the following tests form the core of a robust HPMC 200000 control program.
1. Appearance, odor, and foreign-matter inspection
Before laboratory testing begins, inspect the packaging and powder condition. HPMC should be a free-flowing, uniform powder with no visible contamination, unusual discoloration, hard agglomerates, or signs of water exposure. Damaged bags, broken inner liners, and compacted material deserve attention even when the lot number and documents appear correct.
Appearance is not a release test by itself, but it is an early warning tool. Lumps can indicate moisture pickup during storage or transport. Foreign fibers, black particles, or inconsistent color can point to handling contamination. An unusual odor may suggest that the material was stored near volatile chemicals or that packaging integrity was compromised.
2. Moisture content
Moisture is one of the most operationally important checks. HPMC is hygroscopic to a degree, and excess moisture can reduce powder flow, promote clumping, complicate dosing, and affect the amount of active polymer delivered per kilogram. In dry-mix production, moisture variation also makes it harder to maintain a stable water-demand profile from batch to batch.
Use a validated moisture method appropriate for cellulose ether, such as loss on drying under controlled conditions or another internally approved technique. The key is consistency: the same drying temperature, sample mass, timing, and calculation method should be used for incoming samples and retained controls.
When a moisture result trends upward but remains within the formal limit, do not ignore it. Review warehouse humidity, pallet protection, bag sealing, container unloading practices, and stock rotation. Trend data often reveals a storage issue before it becomes a rejected lot or a production stoppage.
3. Viscosity of the prepared solution
Viscosity is the defining performance test for HPMC 200000, but it must be performed with care. High-viscosity grades do not hydrate instantly. Poor dispersion, insufficient standing time, trapped air, or incomplete dissolution can produce misleading results.
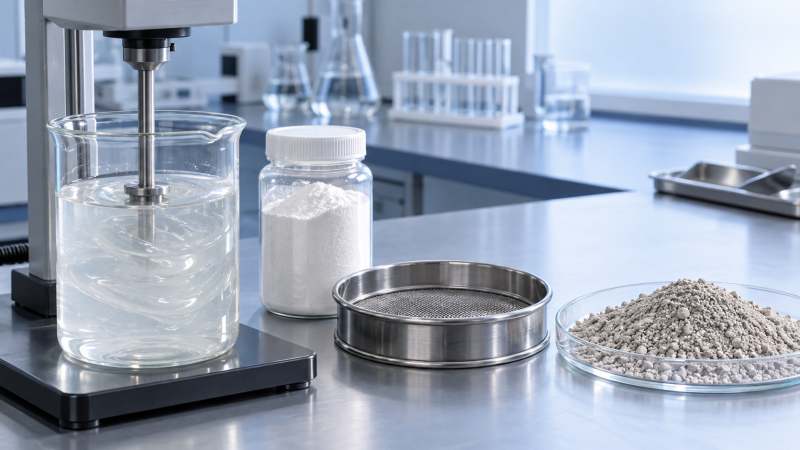
A controlled preparation procedure should specify the water quality, powder addition rate, mixing speed, temperature sequence, hydration period, and de-aeration approach. Many laboratories disperse HPMC in hot water and complete dissolution during cooling, while others use an approved cold-water dispersion process. Whatever method is selected, it should be repeatable and aligned with the supplier’s technical guidance.
Beyond the final number, observe the solution itself. A properly prepared solution should be uniform and free from persistent gel particles, dry cores, or visible insolubles. If a result falls outside the normal range, repeat the test from a fresh sample preparation before making a release decision. Then compare the sample against a retained lot under identical conditions.
4. pH of the aqueous solution
The pH test is fast, inexpensive, and useful for detecting unusual chemical variation. Although HPMC is generally regarded as a nonionic cellulose ether, the pH of its solution may still influence compatibility with other mortar ingredients and can indicate an abnormal production or contamination event.
Measure pH at the defined solution concentration and temperature. A slight variation may be acceptable, but a sudden departure from the established control band should trigger investigation. In dry-mix systems, pH-related concerns are rarely isolated; they may become more meaningful when combined with unexpected viscosity behavior, ash changes, or application-test deviations.
5. Particle-size distribution and sieve residue
Particle size affects how quickly HPMC disperses into water and how reliably it blends with cement, sand, fillers, and other powdered additives. Fine particles may hydrate rapidly but can generate dust and form surface gels if introduced to water too quickly. Coarser particles can disperse more slowly and may leave undissolved specks if the mixing procedure is not adequate.
For routine control, sieve analysis or residue-on-sieve testing may be sufficient. More detailed particle-size analysis can be valuable when a formulation is particularly sensitive to dissolution speed or when the material is processed through high-speed dry blending equipment. The point is not to impose a universal particle-size target; it is to maintain consistency with the grade that was validated in the mortar recipe.
6. Ash content
Ash content provides insight into inorganic residue remaining after controlled ignition. It can be a useful indicator of purity, process consistency, and possible contamination. An unexpected increase may affect mortar color, alkalinity balance, or interaction with other additives, depending on the formulation.
This test is especially valuable as a trend-control tool. A single compliant result does not always tell the whole story, while a gradual shift across multiple deliveries may indicate a meaningful change in raw materials or manufacturing conditions. Quality teams should review ash results alongside viscosity and solution appearance rather than treating each parameter as completely independent.
7. Dissolution behavior and gel-particle observation
Dry-mix mortar producers do not use HPMC in a laboratory beaker; they use it in a dynamic system where water, mineral binders, fillers, and mixing energy arrive together. A simple dissolution or hydration assessment helps bridge that gap.
Prepare the sample according to a controlled procedure and record the time needed to obtain a homogeneous solution. Look for fish eyes, agglomerates, floating powder, or persistent gel particles. These observations are particularly relevant after a change in particle size, packaging condition, or production source.
For higher-risk applications, an internal “wet-mix screening test” can be added. A small standardized mortar batch can be evaluated for water demand, mixing time, consistency development, and visual homogeneity. It does not replace full formulation validation, but it can prevent a questionable lot from moving directly into large-scale production.
Why Batch Consistency Deserves Its Own Control Point
Many quality failures are caused not by one clearly defective parameter, but by several small deviations occurring together. A lot may be near the lower side of the viscosity range, slightly higher in moisture, and slower to dissolve than the retained reference. Each value may appear acceptable alone. In a demanding tile adhesive or wall putty formulation, their combined effect can still be noticeable.
For this reason, batch consistency should be assessed through trend review, not only pass/fail limits. Build a lot history for viscosity, moisture, pH, ash, and sieve residue. Compare new deliveries with the approved reference sample and with recent production experience. Control charts are helpful because they distinguish ordinary variation from a gradual process drift.
Linking HPMC Testing to the Rest of the Formulation
HPMC does not work in isolation. Its performance depends on the binder system, filler loading, sand grading, retarders, accelerators, starch ether, and polymer modifiers present in the formula. A change in cellulose ether behavior may be amplified or partially masked by these other components.
For example, a formulation containing Redispersible Polymer Powder may show a different balance between workability, adhesion, and water retention than an unmodified mortar. If a production team changes either polymer powder or HPMC source, the safest practice is to review the combined system rather than approving each raw material only through isolated tests.
This is particularly important for quality teams handling formulation changes. A compliant HPMC 200000 lot should not automatically be assumed interchangeable with another high-viscosity grade. Substitution decisions should consider viscosity method, substitution level, particle size, hydration behavior, and trial-mix results under the actual plant mixing conditions.
A Practical Release and Escalation Workflow
A reliable control system does not need to be complicated, but it must be clear enough that different shifts reach the same decision. On receipt, verify the supplier name, product code, batch number, manufacturing date, packaging condition, and certificate documentation. Sample according to an approved plan that represents the delivery, rather than taking powder only from the top of one bag.
Run the fast checks first: appearance, moisture, pH, and basic sieve condition. Then complete viscosity and dissolution tests under controlled laboratory conditions. Compare the results with the approved specification and retained reference data. If any value is borderline, hold the lot while a repeat test, second sample, or small mortar screening test is completed.
Do not release material based solely on a supplier certificate when internal observations disagree. Certificates are important traceability documents, but they do not replace incoming verification. Likewise, avoid rejecting a lot on one anomalous laboratory reading without checking sample preparation, instrument calibration, and analyst procedure. Good quality control is evidence-based, not reactive.
Safety Considerations During Sampling and Testing
Although HPMC is widely handled as a construction additive, fine organic powders still require appropriate dust control. Sampling, sieving, and transfer operations can create airborne particles. Use local extraction where available, keep containers closed when not in use, and follow site requirements for respiratory protection, eye protection, gloves, and housekeeping.
Prevent powder accumulation around electrical equipment and avoid unnecessary ignition sources in dusty work areas. Laboratory personnel should also be trained in safe hot-water handling when solution preparation requires elevated temperatures. Safety records, cleaning routines, and sample-retention practices should be integrated with the quality system rather than treated as separate paperwork.
What a Good Supplier Relationship Adds to Control
Internal testing is essential, but it works best alongside transparent technical communication. Suppliers should be able to provide consistent product identification, test-method information, batch documentation, and guidance on storage and solution preparation. For producers working with broad construction-grade viscosity ranges, method alignment is especially important.
Jinan Ludong Chemical Co., Ltd. manufactures cellulose ethers for construction and chemical applications, including HPMC grades with controlled viscosities from lower ranges up to 200,000 CPS. For mortar manufacturers, the useful question is not simply whether a product is available at a stated viscosity; it is whether the supplier’s test conditions, packaging, batch traceability, and technical support can be aligned with the plant’s own release standards.
Ultimately, controlling HPMC 200000 means protecting the repeatability that customers feel when they mix a mortar bag with water. A well-designed test plan catches variation before it reaches the mixer, gives safety teams clearer handling controls, and gives production teams greater confidence that each batch will behave like the one approved in the laboratory.
Send Your Inquiry
We welcome your cooperation and we will develop with you.
